 EN
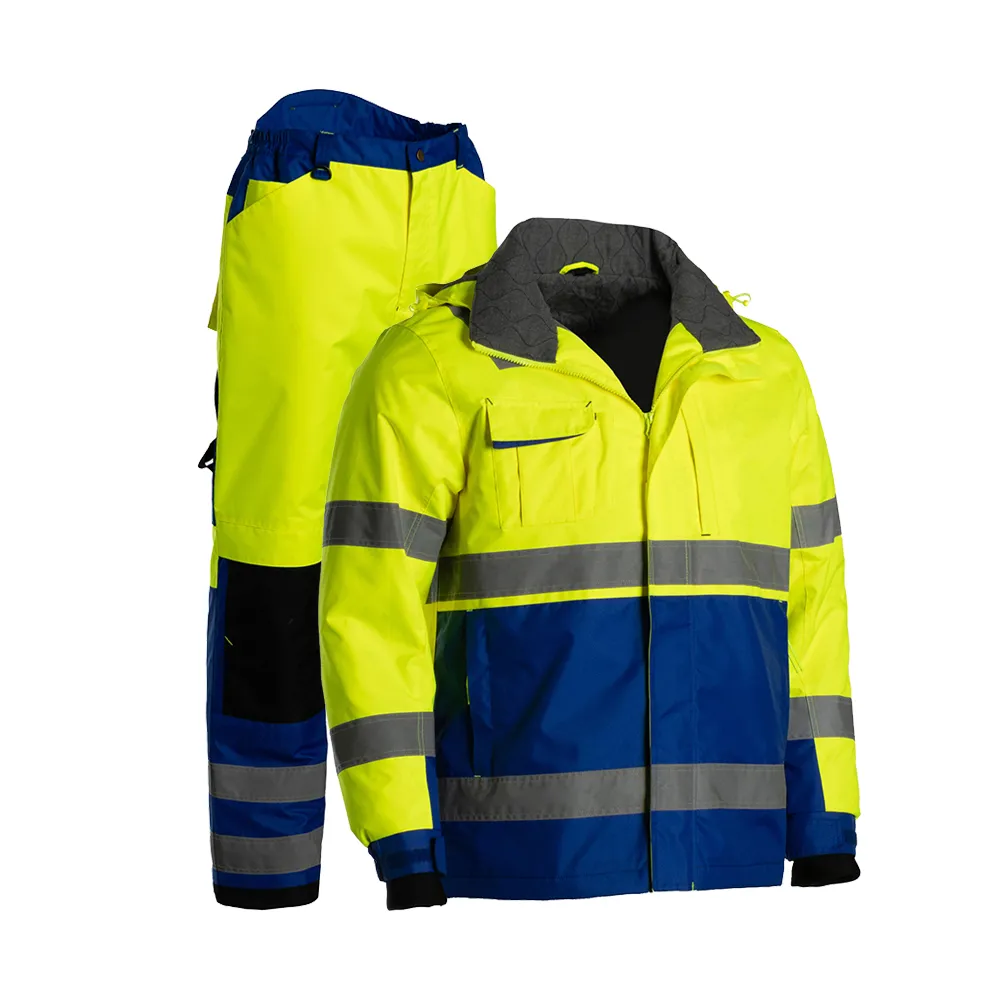
Operating within upstream oil rigs, midstream pipelines, and downstream petrochemical refineries requires navigating some of the most unforgiving working conditions in modern industry. Field operators, maintenance engineers, and safety technicians face constant exposure to volatile hydrocarbons, pressurized lines, and high-voltage electrical networks. Under these high-risk conditions, personal protective gear serves as the absolute last barrier protecting human life from catastrophic burn injuries.
Selecting industrial flame-resistant clothing demands a grounded understanding of thermal physics, fabric engineering, and long-term durability. Buying teams must move past superficial price tag comparisons to evaluate how protective garments handle extreme heat, daily friction, chemical exposure, and endless laundering cycles in real-world environments.
Understanding Thermal Hazards Across Energy Operations
Hydrocarbon processing facilities carry unique thermal risks that develop in fractions of a second. Flash fires during routine processing or pipeline maintenance can instantly escalate temperatures anywhere from 1,000 degrees Fahrenheit up to 1,900 degrees Fahrenheit. The fundamental job of safety workwear is not to magically block all heat forever, but to stop fabrics from igniting, melting onto skin, or continuing to burn once the thermal source subsides.
Preventing severe second and third-degree burn coverage gives workers critical seconds to evacuate danger zones safely. Furthermore, downstream maintenance teams working near high-voltage motor control centers face significant electrical arc flash hazards. An arc flash event releases massive amounts of radiant energy and intense pressure waves, making specialized arc-rated garments essential for electrical safety compliance.
Navigating Global Safety and Compliance Standards
Procurement managers sourcing gear for multi-regional operations must ensure all supplied garments hold third-party certifications rather than relying on self-declared factory claims. Recognizing international testing protocols ensures every delivery lot delivers genuine protection in dangerous field conditions.
Key international compliance standards include:
-
NFPA 2112 Compliance: The core North American standard governing flame-resistant garments for industrial personnel against short-duration thermal exposure. Testing mandates that clothing demonstrates less than 50 percent total predicted body burn in standardized 3-second thermal mannequin trials.
-
NFPA 70E and Arc Ratings: Regulates workplace electrical safety requirements, defining the Arc Thermal Performance Value measured in calories per square centimeter to categorize protective equipment tiers.
-
EN ISO 11612 Compliance: The primary European and international standard assessing protective apparel against convective heat, radiant heat, and molten metal splash risks.
-
EN 1149-5 Anti-Static Standards: Mandates electrostatic dissipative properties to prevent static spark generation inside explosive atmospheric zones.
Material Engineering: Inherent FR Versus Treated Cotton Fabrics
Selecting the core fabric structure represents one of the most critical decisions in establishing a reliable safety wear program. Protective fabrics generally fall into two primary technology paths, each offering distinct operational benefits depending on environmental demands.
Inherent flame-resistant materials incorporate protective chemical structures directly inside the synthetic polymer fibers before spinning into yarns. Fiber blends combining meta-aramids, para-aramids, and modacrylics will never lose their protective capabilities regardless of how many times the garment gets washed or worn. These fabrics deliver exceptional tear strength, outstanding resistance to chemical degradation, and superior longevity in harsh offshore or acid-heavy refinery units.
Treated flame-resistant fabrics utilize natural fibers like heavy cotton or cotton-nylon blends that undergo specialized chemical treatments during finishing phases. Treated cotton options offer excellent natural breathability, superior softness against skin, and lower initial purchase costs. However, buyers must verify that laundry facilities strictly adhere to specified washing guidelines to preserve the chemical protective layer across extended operational lifecycles.
Balancing Thermal Defense with Wearer Comfort and Ergonomics
Thermal protection provides little value if field workers find the garments unwearable during hot summer shifts. In high-temperature operating environments like the Middle East or coastal offshore rigs, heat stress represents a daily operational risk that can prove just as dangerous as sudden flash fire hazards. Heavy, non-breathable gear causes rapid physical exhaustion, leading workers to unbutton collars or roll up sleeves, exposing vulnerable skin to immediate danger.
Modern fabric design focuses heavily on weight reduction, moisture management, and airflow permeability. Utilizing lightweight protective textiles ranging between 4.5 ounces and 7.0 ounces per square yard allows body heat to vent efficiently. Incorporating moisture-wicking channels keeps workers cool and dry without sacrificing the carbonization process that seals out heat during a flash fire event. High-stress garment zones should also feature ergonomic sleeve patterning, triple-needle seam reinforcement, and non-conductive aramid sewing threads to resist abrasion along heavy pipe racks and machinery decks.
Commercial Value and Total Cost of Ownership Evaluation
Smart procurement teams evaluate safety apparel using a Total Cost of Ownership framework rather than basic initial unit cost. A low-cost garment that frays, shrinks, or fades after 30 commercial laundry cycles ultimately costs far more than a premium alternative engineered to survive over 100 industrial washings.
Essential procurement evaluation factors include:
-
Fabric Shrinkage Control: Maintaining dimensional stability below 3 percent to prevent garments from restricting movement after washing.
-
Color Retention Performance: Ensuring high visibility and clean corporate branding across multi-year field deployments.
-
Seam and Closure Integrity: Utilizing heavy-duty non-conductive zippers, reinforced pocket corners, and flame-retardant trim hardware.
-
Garment Standardization: Streamlining sizing profiles to simplify bulk inventory management across diverse workforce demographics.
Building Reliable Supply Chain Partnerships
Establishing an uncompromising safety infrastructure requires collaborating with an experienced manufacturing partner skilled in technical textile engineering, global compliance verification, and dependable logistics execution. Specialized brands like HiWorld deliver fully integrated garment design and supply chain capabilities tailored directly to the oil, gas, and petrochemical industries. Leveraging modern fabric engineering, rigorous quality management systems, and flexible customization services ensures energy field crews remain reliably protected against complex thermal hazards anywhere across the globe.
Table of Contents
- Understanding Thermal Hazards Across Energy Operations
- Navigating Global Safety and Compliance Standards
- Material Engineering: Inherent FR Versus Treated Cotton Fabrics
- Balancing Thermal Defense with Wearer Comfort and Ergonomics
- Commercial Value and Total Cost of Ownership Evaluation
- Building Reliable Supply Chain Partnerships